
Furniture Inspection Sampling and AQL: What Buyers Should Agree Before Inspection
Agree the inspection lot, sampling plan, defect definitions, references and release authority before a furniture inspection. Includes a practical agreement table.
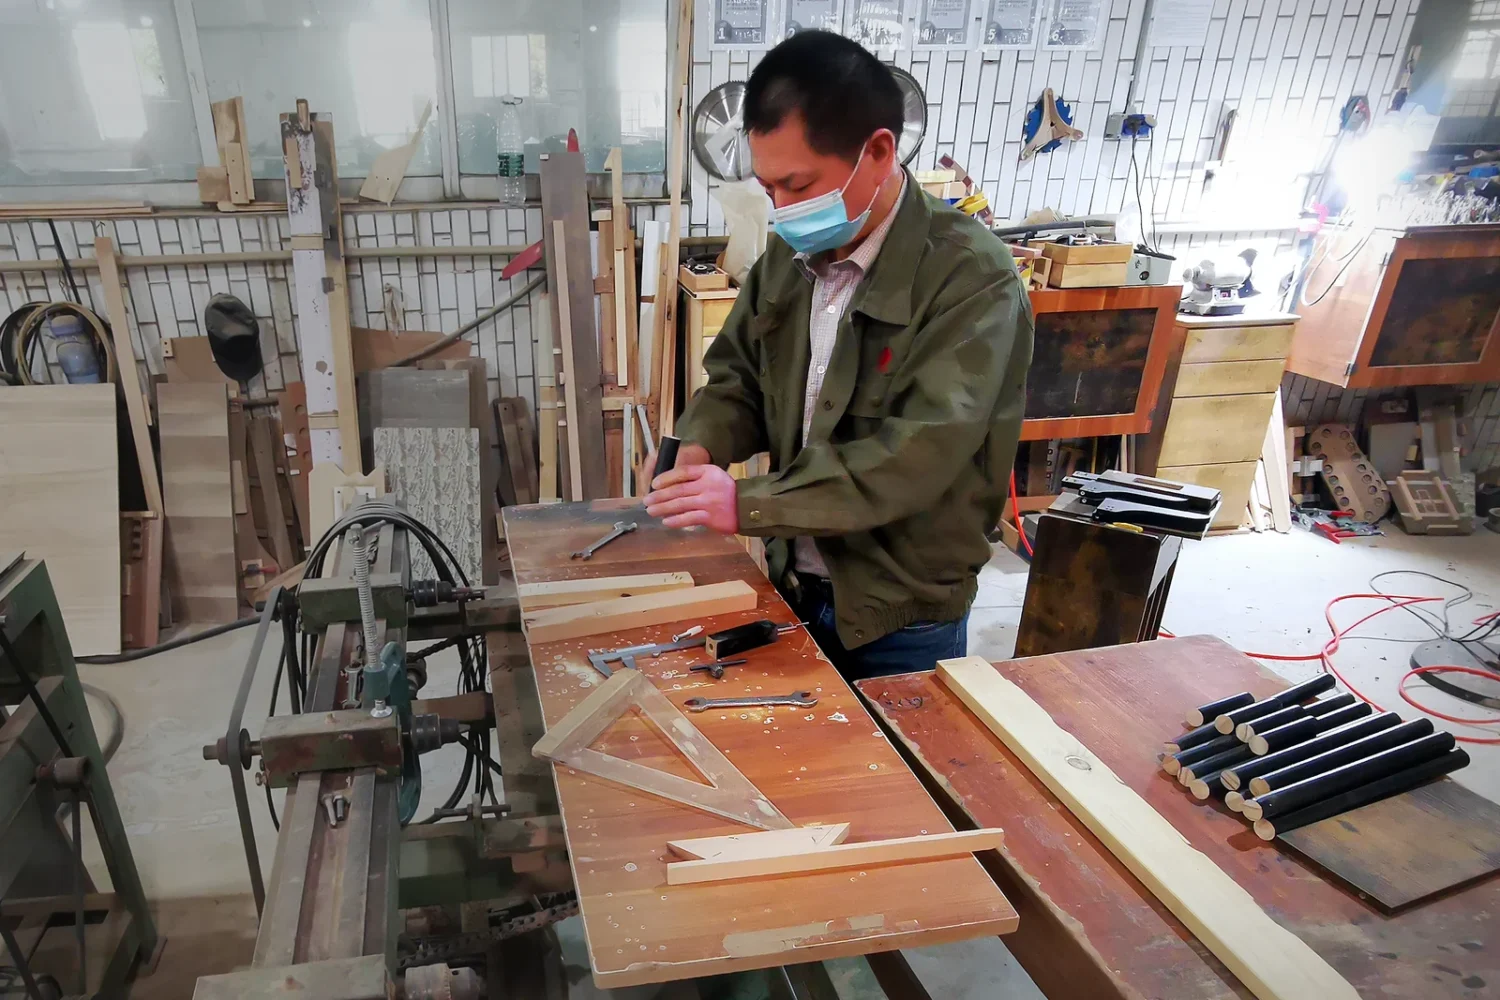
A worker uses a measuring tool on a wooden furniture sample at a workbench.
Before a furniture inspection, agree the lot and inspection unit, applicable sampling standard and edition, defect definitions, approved references, sample selection method, acceptance rules and release authority. An AQL value alone does not tell an inspector what to inspect or a buyer whether to ship.
The practical deliverable is a written inspection instruction that the buyer, supplier and inspection provider can all use. It should make the result reproducible: another reviewer should be able to identify the same lot, understand the findings and follow the same decision rule.
This guide covers those sampling and acceptance agreements. For the actual component, assembly, appearance and pack-out checkpoints, use Furniture Inspection and Quality Control.
What AQL Does—and Does Not—Tell a Furniture Buyer
AQL means Acceptance Quality Limit. In an AQL-indexed sampling scheme, it is a parameter used to select the acceptance arrangement. It is not a promise that every accepted shipment contains no more than that percentage of nonconforming furniture, and it is not permission to knowingly supply defective units.
Acceptance sampling uses findings from a selected sample to make a decision about a defined lot. It leaves sampling risk: an accepted lot can still contain nonconforming units. NIST explains that its main purpose is a lot acceptance decision, rather than estimating the lot’s actual quality. See NIST’s introduction to acceptance sampling.
A zero acceptance number does not guarantee a defect-free lot. It requires no findings of the counted category in the sample under that plan; uninspected units can still contain problems. The probability of acceptance depends on the plan and the underlying lot quality, as explained in NIST’s discussion of operating characteristic curves. Do not translate “none found” into “none exist.”
Define the Lot, the Unit and the Variant Coverage
A purchase order, a container and an inspection lot need not be the same thing. Identify the actual stock offered for inspection: order reference, production or batch references where available, product revision, quantities, location and readiness. Record exclusions, unfinished stock and quantities that are not accessible.
Define the inspection unit explicitly. For a flat-pack cabinet, is it one complete saleable set, one carton, one panel or one hardware pack? If one saleable set uses multiple cartons, explain how the cartons will be paired. Counting cartons as complete products can hide missing parts of a set and change the meaning of the lot size.
For mixed-SKU or mixed-finish orders, list each variant and quantity before agreeing coverage. Decide whether they will be separate lots or part of a documented grouping that is suitable for the chosen scheme and characteristics. Different construction, finish requirements or production histories can be reasons to keep results separate. A shared container or similar product name is not a sufficient grouping explanation.
If a plan combines variants, state how each is represented and how its findings affect the decision. Do not let a small variant disappear inside a larger sample dominated by another finish. Conversely, do not describe a few extra checks on that variant as a separate statistical acceptance decision unless an appropriate plan has actually been defined.
Record the Standard and the Complete Sampling Arrangement
Name the standard and edition in the inspection instruction. As of November 2026, ISO lists ISO 2859-1:2026, third edition, for AQL-indexed inspection by attributes. ASQ’s public overview lists ANSI/ASQ Z1.4-2003 (R2018). Do not combine an ISO edition, an older supplier worksheet and an online calculator without checking that they implement the agreed scheme.
Also record whether the arrangement is single, double or multiple sampling; the inspection level; the applicable normal, tightened or reduced inspection state; and the AQL and counting basis for each agreed category. Inspection level and inspection state are separate choices. These schemes include rules for their use over a sequence of lots, so ask the plan preparer to confirm suitability for an isolated order or a new supply programme and identify the required history and switching rules.
Inspection level is not the sample size, and sample size is not the acceptance number. In table-based arrangements, lot size and inspection level lead into the sample selection process; the selected scheme, inspection state, AQL and table instructions determine the applicable sample and decision limits. Where a code letter is used, record it together with the final sample size and acceptance/rejection numbers. ASQ’s worked explanation of sample selection illustrates why table directions matter; its older numerical example should not be substituted for the edition in your contract.
Have the inspection provider supply the completed plan and its reference before the visit. Neither a fixed percentage of the order nor a familiar AQL value is a complete instruction. This guide does not prescribe default AQL values or reproduce sampling tables.
Agree What Counts Before Counting It
Build a defect catalogue around the product’s approved requirements. For each finding, identify the affected feature, decision criterion, severity category and evidence needed. If using labels such as critical, major and minor, define their meaning for this order. A scratch on a customer-facing surface and a mark on a concealed surface need not receive the same classification; the agreed criteria should resolve the difference.
For dimensions, name the measurement points, units, tolerance and method. For appearance, identify the finish reference and viewing conditions. For function, identify the operation to perform and what constitutes failure. Assign a controlling reference to each requirement: a drawing revision, specification, approved physical sample, finish sample, manual or packaging instruction. Resolve conflicts between them before making a pass/fail decision.
Separate nonconformities from nonconforming units. A nonconformity is an individual departure from a requirement; a nonconforming unit is an item with one or more such departures in the category being counted. ASQ distinguishes schemes based on percent nonconforming from those based on nonconformities per hundred units in its attributes sampling overview.
For example, suppose one cabinet has two separately reportable scratches and a missing fitting, all assigned to the same category in a hypothetical defect catalogue. That is three nonconformities but one nonconforming cabinet in that category. Record every finding, then apply the agreed unit-counting rule. Also specify how units with findings in more than one severity category enter each tally; do not silently add category totals and call the sum a count of distinct defective products.
A Compact Pre-Inspection Agreement
Use this as the cover sheet for the inspection instruction, with the detailed specification and sampling plan attached. It is a buyer planning aid, not a replacement for the selected standard.
| Agreement | What to record |
|---|---|
| Lot and unit | Stock identity, location, ready quantity, exclusions and whether the counted unit is a complete set, carton or component. |
| SKU / variant scope | Quantities by variant; separate lots or justified grouping; coverage and decision treatment for each group. |
| Sampling plan | Standard and edition, plan type, level, inspection state, counting basis and AQL by category; confirmed sample size and Ac/Re; applicable switching rules. |
| Defect criteria | Severity definitions, defect catalogue, tolerances, controlling references and approved revisions; how repeated and cross-category findings are counted. |
| Selection and access | Random selection procedure, stock access, carton/set identification and how unavailable or substituted selections will be recorded. |
| Check coverage | For each appearance, dimension, function and packaging check: method, sample count, unit IDs, decision rule and any separate test scope. |
| Failure and reinspection | Hold scope, correction owner, affected-stock review, resubmission identity, reinspection plan, cost and timing responsibilities. |
| Decision authority | Who reports, who accepts the lot, who can approve a defined concession, who releases shipment and who acts if a decision remains unresolved. |
Select Samples from the Agreed Stock and Preserve the Findings
Arrange access to the whole defined lot so that selection can follow the agreed random procedure. Record where selected units came from and retain carton or unit identifiers through opening, assembly and reporting. Supplier-prepared display samples should not silently replace the production sample.
If selected stock is inaccessible, record the restriction and obtain a decision about restoring access, rescheduling or revising scope. Do not substitute convenient cartons without explanation and retain the original full-lot conclusion.
For a conventional single-sampling count plan, compare the completed sample tally with the specified acceptance number (Ac) and rejection number (Re): a count at or below Ac meets that category’s acceptance rule; a count at or above Re meets its rejection rule. All applicable categories and other agreed release conditions still need to be addressed. Double or multiple sampling may require another prescribed stage and combined results; follow the selected plan’s rules. NIST describes these different plan structures.
Keep the original findings even if an item is repaired during the visit. Replacing a failed sample with a good unit and deleting the failure changes the evidence. An extra sample taken simply to obtain a better result is not the same as the next stage of an agreed sampling plan.
Do Appearance, Function, Dimensions and Packaging Use the Same Sample?
They can share selected units where practical, but do not assume they share the same sample size, method or decision rule. Opening every selected carton for appearance is different from assembling selected complete sets, measuring specified interfaces or carrying out a destructive test.
List each check separately in the instruction and report its actual coverage. If fewer units receive a functional or dimensional check, show that count and the agreed basis. An unperformed check should remain “not checked,” rather than inheriting a pass from the visual inspection. Record which units receive several checks so their findings remain traceable.
Using a measuring tool does not automatically make a check a statistical variables plan: measurements may simply be compared with tolerances and counted as conforming or nonconforming. Agree that treatment explicitly.
Sampling acceptance for appearance cannot replace applicable safety testing or compliance obligations. Keep those requirements and evidence gates separate from the visual tally. The distinction is covered in QC vs Product Testing vs Compliance; when a laboratory report is part of the release file, use Verify a Furniture Test Report to review its scope.
Hypothetical Example: Two Finishes, Conflicting References
Illustrative scenario only—not a HOMVND order or customer case. A buyer orders flat-pack side tables in light and dark finishes. The inspection instruction treats the finishes as separate lots and counts nonconforming complete sets by severity. The dark-finish stock carries a revised finish reference, but the inspector receives an earlier approved sample.
The inspector finds a colour difference and a drawer that binds on one dark-finish set. A scratch is also recorded on that set. The supplier proposes using the earlier finish sample and removing the drawer finding after adjustment.
- Keep the observations. Identify the set, photograph the colour and scratch, and record the drawer behaviour before and after adjustment. The adjustment does not erase the initial finding.
- Resolve the reference conflict. The buyer’s named quality decision-maker checks the approval trail and confirms which finish reference governs this stock. Until that is settled, the colour judgement remains unresolved. Other valid checks can continue.
- Apply the agreed counting basis. If the confirmed catalogue assigns the drawer and scratch findings to the same category, retain both findings but count the affected set once in that category. Classify the colour finding only after resolving its reference.
- Decide within the original scope. Compare each finish lot’s completed tally with its agreed plan. Do not dilute the dark-finish findings with passing light-finish units. If partial shipment is considered, separately document the released lot, quantities and remaining hold.
No sample size or Ac/Re values are assumed here. The point is to preserve the lot boundary, reference decision and counting rule before using the actual agreed limits.
Separate the Inspection Result from the Shipment Decision
Before inspection, name the people who can make each decision. The inspector records findings and the result against the instruction. The supplier owns the agreed corrective work. The buyer’s designated authority accepts or rejects the proposed disposition; shipment release may require an additional commercial or compliance approval.
For a non-accepted lot, identify and hold the affected stock, record the failure basis, and agree the correction and evidence needed before resubmission. Address the affected lot, not just the faulty units found in the sample. Depending on the issue, the agreed action may involve sorting, rework, replacement or return. Record responsibility, costs and timing.
Reinspection should identify the resubmitted stock, completed actions, revised quantities if applicable, reference versions and the applicable sampling arrangement. Link the new report to the original failure and retain both results. The scope of reinspection should address the failure and any other characteristics affected by the corrective work.
If an authorized buyer accepts a defined deviation, record it as a concession: exact lot and quantity, requirement waived, reason, conditions, approver and date. Keep the original inspection result visible. A concession is not a new general tolerance, and a commercial approval cannot waive applicable safety or legal obligations.
A useful release record answers four questions: which stock, against which rules, with which unresolved or corrected findings, and approved by whom? Attach that record to the inspection report so that “accepted,” “reworked,” “awaiting decision” and “released for shipment” cannot be mistaken for the same status.